To meet the demands and ensure compliance with all legal requirements of regulatory bodies, it is essential that food industries have an efficient management platform capable of controlling and monitoring each stage of the quality process in an integrated and precise manner.
Challenges and Solutions
Strict sanitary and regulatory requirements
Challenge
Difficulty in meeting the standards of ANVISA (Brazilian Health Regulatory Agency), MAPA (Brazilian Ministry of Agriculture, Livestock and Supply), and certifications such as ISO 22000 and HACCP.
Solution
OPEN Manufacturing ensures complete traceability, auditable records, and automated control, facilitating inspections and audits.
Expiration date control and storage of perishable products
Challenge
Losses due to batch expiration or failures in the preservation of raw materials and finished products.
Solution
Monitoring of temperature, expiration dates, and storage conditions, with automatic alerts to prevent losses and preserve quality.
Recipe management and formulation standards
Challenge
Inconsistency in production due to failures in recipe and proportion control.
Solution
Standardized control of formulas and quantities, with traceability by batch and production history, ensuring the uniformity of the final product.
Traceability of ingredients and batches
Challenge
Difficulty in quickly identifying the source of problems in the event of a recall.
Solution
End-to-end traceability, from supplier to consumer, with detailed control of batches, dates, and production processes.
Excessive waste of raw materials and supplies
Challenge
High costs due to losses in processes such as mixing, filling, and packaging.
Solution
Real-time monitoring of production stages, with precise control of consumption, losses, and efficiency at each stage.
Production control by shift and by line
Challenge
Lack of visibility into line performance and team productivity.
Solution
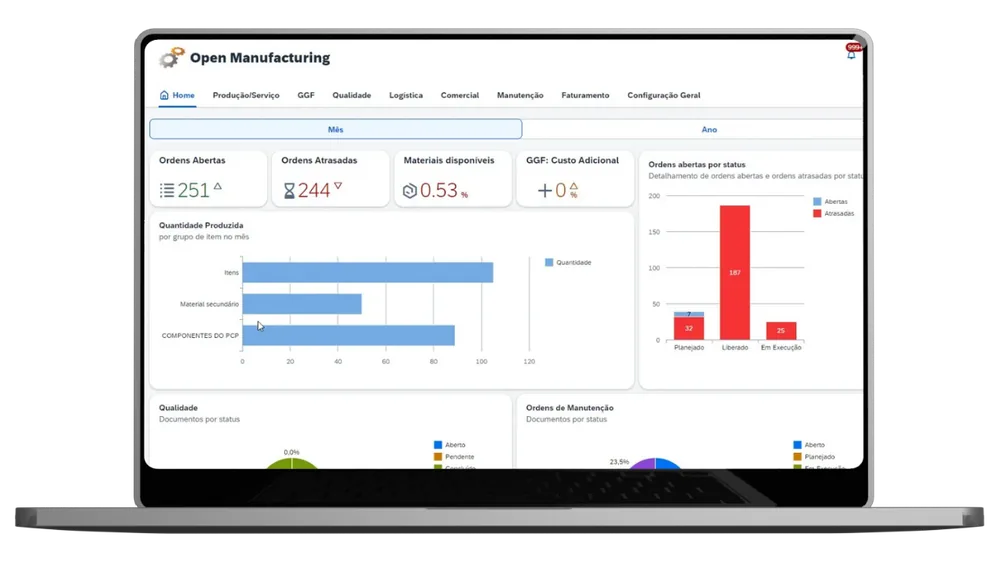
Real-time dashboards displaying indicators for production, line throughput, shift efficiency, and losses, facilitating quick decision-making.
Handling requests with high variability and seasonality
Challenge
Difficulty in planning production in the face of peak demand and varied products.
Solution
Integrated planning and MRP that adjust production based on demand forecasting, seasonality, and production capacity.
Pressure for tighter margins and increased competitiveness
Challenge
Rising costs and competition demand complete control of operations.
Solution
A centralized and strategic view of the entire operation, with integrated data on cost, productivity, losses, and profitability by product or line.
We specialize in developing solutions for MANUFACTURING INDUSTRIES, transforming technology into real results
Take your production to the next level
Your smartest, most connected, and most strategic factory.
Integrated Processes
Agile Production
Advanced Management
Strategic Solutions
OPEN Manufacturing
Our solution has modules that meet the needs of the agribusiness sector and optimize the entire production chain — from receiving raw materials to the final product.
Process Order
Planning, releasing, and monitoring production orders with complete control over inputs used, process times, time tracking, and batch traceability.
MES
It connects the factory floor with real-time management systems, allowing for monitoring of line efficiency, machine performance, losses and downtime, among other factors.
Logistics
It includes picking and packing functionalities, optimizing the separation and shipping of finished products.
Maintenance
The module includes corrective, preventive, and predictive maintenance plans. This reduces downtime and increases the operational availability of the machines.
Quality Control
It allows for the recording of deviations, issuance of reports, and control of rework, with a focus on safety and compliance.
 Português
 Español