 Português
 Español

How maintenance directly influences production efficiency
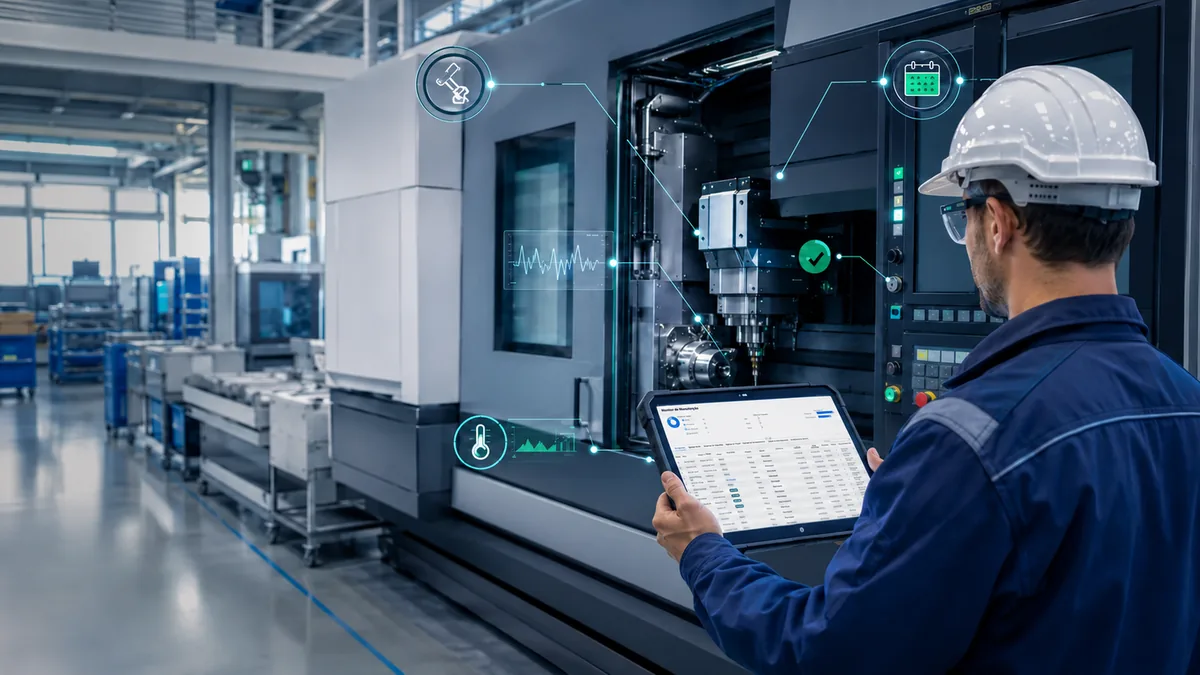
In manufacturing, a machine rarely stops "on its own." When a piece of equipment fails, it can also stop the team, the production line, the flow of orders, shipping, and in some cases, even the customer's confidence in the promised deadline.
Therefore, the industry needs to see maintenance as something bigger than just a department activated when a machine breaks down. It directly influences productive efficiency and determines how much of the installed capacity actually translates into approved products, delivered on time and at a controlled cost.
The question, therefore, is not just how much maintenance costs, but rather: How much does it cost to produce without a well-structured maintenance strategy?
Productive efficiency begins before the machine even starts operating
Productive efficiency is the ability to transform materials, time, energy, people, and equipment into useful output, reducing losses and maintaining quality standards. In practice, it depends on three basic conditions:
- The equipment needs to be available when production requires it;
- It needs to operate at the expected speed and under the expected conditions;
- You need to deliver products that meet specifications.
Note the central point: all three factors are directly related to maintenance.
An obvious failure reduces availability. Even component wear, while not interrupting the machine, can slow down the process. Furthermore, misalignments, clearances, temperature variations, excessive vibration, or uncalibrated instruments can lead to defects, rework, and loss of raw materials.
In other words, not all losses caused by maintenance appear as a major shutdown. Many are hidden in slower cycles, micro-stoppages, frequent adjustments, excessive consumption, and quality variations. The line continues to operate—but it's working below its potential.
The relationship between maintenance and OEE
One of the most widely used indicators for evaluating equipment productivity is OEE — Overall Equipment Effectiveness. Its logic combines three factors:
OEE = Availability × Performance × Quality
This formula helps to understand why maintenance and production cannot work as isolated areas.
Availability
It measures how much time the equipment actually spent operating in relation to the planned time. Breakdowns, waiting for parts, delays in diagnosis, and prolonged corrective interventions reduce this index.
Performance
Compare the actual production rate with the projected rate. Worn equipment, inadequate adjustments, and recurring minor interruptions cause the operation to produce more slowly, even without a long stoppage.
Quality
Consider how much of the production completed was approved. Mechanical failures, unstable parameters, and components out of condition can lead to increased scrap, rework, and process deviations.
Thus, efficient maintenance doesn't "just fix machines." It protects the three pillars of OEE and helps transform nominal capacity into real productive capacity.
The domino effect of an unplanned shutdown
Imagine a production order scheduled to finish in the first shift. Suddenly, a failure interrupts the critical equipment on the line. Maintenance receives the information late, searches the machine's history, identifies the need for a component, and waits for it to be located in inventory.
Meanwhile, the schedule needs to be redone. The team is idle or reassigned. The next batch loses its production window. Shipping is under pressure, and sales needs to renegotiate delivery.
Now visualize the same event with integrated processes: the system records the stoppage the moment it occurs, associates the reason with the equipment, and generates a maintenance order. At the same time, the team accesses the asset's history and monitors the intervention with reliable information.
Failure remains undesirable, but its duration and impact may be less. This difference between react to the problem e respond to the problem with process and data. It is one of the foundations of productive efficiency.
Corrective, preventive, and predictive: which strategy is most efficient?
In this context, there is no single approach suitable for all assets. The best results usually come from combining strategies according to criticality, risk, cost, and equipment behavior.
Corrective maintenance
The team performs corrective maintenance after identifying the fault. This strategy can work for simple, redundant, low-cost assets with no significant impact on safety, quality, or production. The problem arises when emergency corrective maintenance becomes the standard for critical equipment.
In this scenario, the factory starts managing emergencies: it buys parts without planning, redeploys teams, alters schedules, and deals with greater operational uncertainty.
Preventive maintenance
The team performs preventive maintenance according to predefined criteria, such as time, cycles, mileage, or production volume. Thus, scheduled inspections, adjustments, and replacements help reduce the probability of failure.
When well-planned, it allows for negotiating the best timeframe with the production planning and control (PPC) department, preparing materials and labor, and preventing a scheduled intervention from turning into an emergency. However, poorly defined schedules can lead to excessive or insufficient maintenance. Therefore, the asset's history is essential for reviewing the plans.
Predictive maintenance
In turn, predictive maintenance considers the actual condition of the equipment. Data on vibration, temperature, pressure, electrical current, noise, lubrication, and other variables help identify degradation trends.
In this way, the team can intervene at the technically appropriate time, before functional failure, but without prematurely replacing components. Sensors help with this, but they don't work miracles. The operation also needs to guarantee data quality, analysis criteria, historical data, and a workflow capable of transforming alerts into action.
Interesting fact: maintenance also influences quality
At first glance, many people associate maintenance only with breakdowns and stoppages. However, a study by the National Institute of Standards and Technology (NIST) of industrial establishments in the United States found an association between greater adoption of predictive maintenance and better operational results. Among companies that already primarily used preventive and predictive maintenance, the group with more intensive use of predictive maintenance was associated with 15% less downtime and an 87% lower defect rate.
These numbers don't represent a universal promise, as they vary according to process, maturity, and sector. Still, the relevant conclusion remains: maintenance, quality, and productivity are measurably connected.
In another case published by NIST's Manufacturing Extension Partnership program, a CNC lathe operation recorded an approximate increase of 22% in productivity after implementing Total Productive Maintenance practices. Furthermore, OEE improved from 39% to 45%. This is a specific case, not a rule for the entire industry, but it demonstrates how small improvements in availability and routine can free up already installed capacity.
The hidden costs of reactive maintenance
The cost of a failure is not limited to the replaced part and the technician's hours. Therefore, a thorough analysis must also consider:
- Production not carried out during the shutdown;
- loss of performance before complete failure;
- Waste and rework generated by instability;
- Overtime and team restructuring;
- emergency purchases and special freight;
- Order rescheduling and delivery delays;
- Additional inventory created as a hedge against instability;
- accelerated wear of related components;
- security risks and impact on the asset's lifespan.
This explains why "saving on maintenance" can be costly. The cut appears immediately in the budget; however, the loss spreads throughout production and appears in different cost centers. In other words, it's the old "cheap is expensive" approach—now with digital tracking and order numbers.
Indicators that connect maintenance and production
To transform maintenance into efficiency, it's necessary to monitor indicators that lead to action. Among the most important are:
- MTBF (Mean Time Between Failures): Mean time between failures; helps assess reliability;
- MTTR (Mean Time To Repair): Average repair time; shows responsiveness and recovery capacity;
- Asset availability: percentage of time the equipment was able to produce;
- percentage of planned maintenance: It reveals how much of the work is planned;
- Compliance with the preventive plan: It indicates whether the planned activities were completed on time;
- Maintenance backlog: Backlog of pending work, preferably analyzed by criticality;
- recurrence of failures: Identifies recurring problems that require root cause analysis;
- OEE: consolidates the effects on availability, performance, and quality.
The indicator alone, however, does not solve the problem. For example, a low MTTR may seem positive, but it can hide quick and recurring repairs that do not eliminate the root cause. Therefore, the team needs to look at the data as a whole and within the operational context.
How can OPEN Manufacturing support this evolution?
OPEN Solutions structured the OPEN Manufacturing Industrial Maintenance Module to support the planning and execution of maintenance activities in an integrated manner with SAP. According to the official presentation of the solution, the platform allows the creation of preventive plans, the management of corrective orders, real-time data entry via mobile devices, and the maintenance of asset history by equipment.
In industrial settings, these resources help organize the entire cycle:
- Plan: Define preventive activities and organize resources before intervention.
- To execute: Record maintenance actions directly in the operational workflow.
- Track: Maintain a history of equipment and incidents.
- To analyze: Identify recurring patterns, timing, causes, and opportunities for improvement.
- Enhance: Adjust plans and priorities based on the actual behavior of the assets.
Furthermore, integration with the MES Module is one of the most relevant points. According to OPEN Solutions, recorded stoppages due to maintenance can automatically generate a maintenance order. This allows the event occurring on the factory floor to reach the responsible team more quickly, reducing communication delays and preserving traceability.
In turn, MES offers real-time data entry and comparisons between planned and actual results. This allows managers to see how failures, micro-stoppages, and interventions affect production execution. The Industry 4.0 Module, in turn, expands this view through the collection of data from machines and sensors. Consequently, the operation obtains information that can support predictive maintenance applications.
Therefore, the value is not simply in digitizing an order that was previously on paper. The gain occurs when maintenance, production, and management start working within the same context, transforming occurrences into historical data and historical data into better decisions.
Efficient maintenance means recovered productive capacity
Before investing in a new machine to expand production, it's worth asking an uncomfortable—and quite profitable—question: How much of the current equipment capacity is lost by the factory due to failures, low speed, micro-stoppages, and quality problems?
Often, some of the desired growth is already inside the factory, hidden in unavailable assets, poorly planned interventions, and disconnected information.
When maintenance moves beyond emergency response and becomes integrated into planning, the company gains predictability. With real-time records, management gains visibility. By integrating production, MES, maintenance, and SAP, the organization also gains speed in decision-making.
As a result, the operation becomes more reliable, makes better use of assets, reduces improvisation, and increases its ability to meet the plan.
Can your company identify, in just a few minutes, which failures most compromised production in the last month? If the answer still relies on scattered spreadsheets, notes, or the team's memory, there is a real opportunity for improvement.
Get to know…
Explore the Industrial Maintenance Module of OPEN Manufacturing and discover how to integrate planning, execution, and data to make maintenance a true pillar of productive efficiency.
I want to meet I want a free demo